In today’s industrial landscape, effective air purification and wastewater treatment solutions are not just regulatory requirements but essential components of sustainable operations. As a premier honeycomb activated carbon manufacturer, Jiangxi Jialin Carbon Technology Co., Ltd. has established itself as a trusted partner for businesses worldwide seeking high-quality activated carbon products and solutions.
With over 20,000 tons of annual activated carbon production capacity and 80,000 cubic meters of honeycomb carbon output, our company stands among China’s largest manufacturers in this specialized field. This impressive scale is matched by our commitment to quality, innovation, and customer service, making us the preferred choice for industrial clients across various sectors.
Understanding Honeycomb Activated Carbon: The Industrial Powerhouse
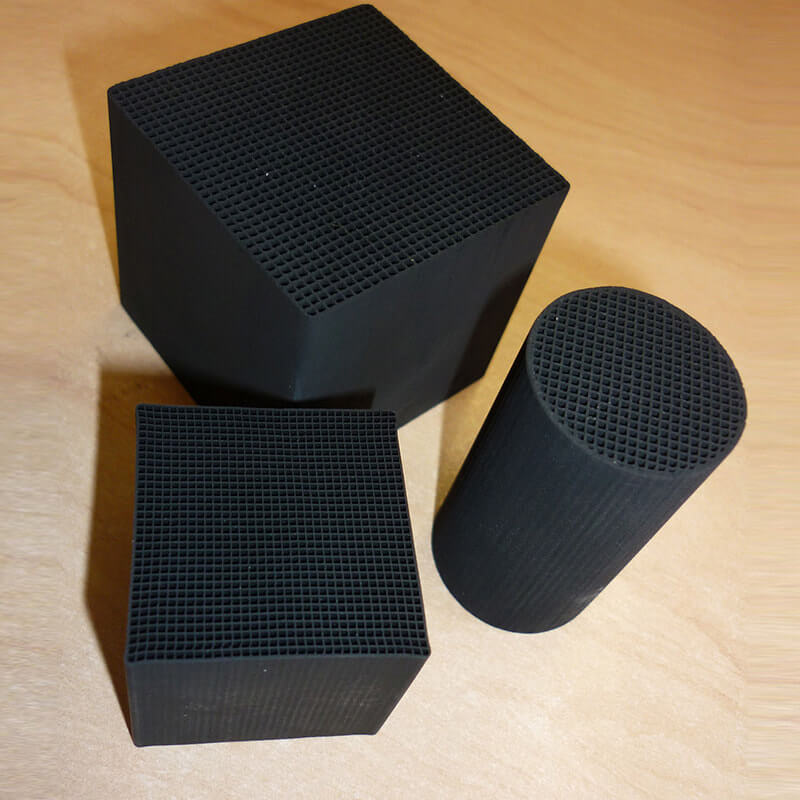
Honeycomb activated carbon represents a significant advancement in filtration technology. Its unique structure combines low air resistance with superior adsorption capacity, making it ideal for treating large volumes of air or gas with low concentrations of contaminants. This characteristic has made our honeycomb carbon products indispensable in industries such as coking plants, chemical factories, printing and dyeing mills, plastic manufacturing, and paper mills.
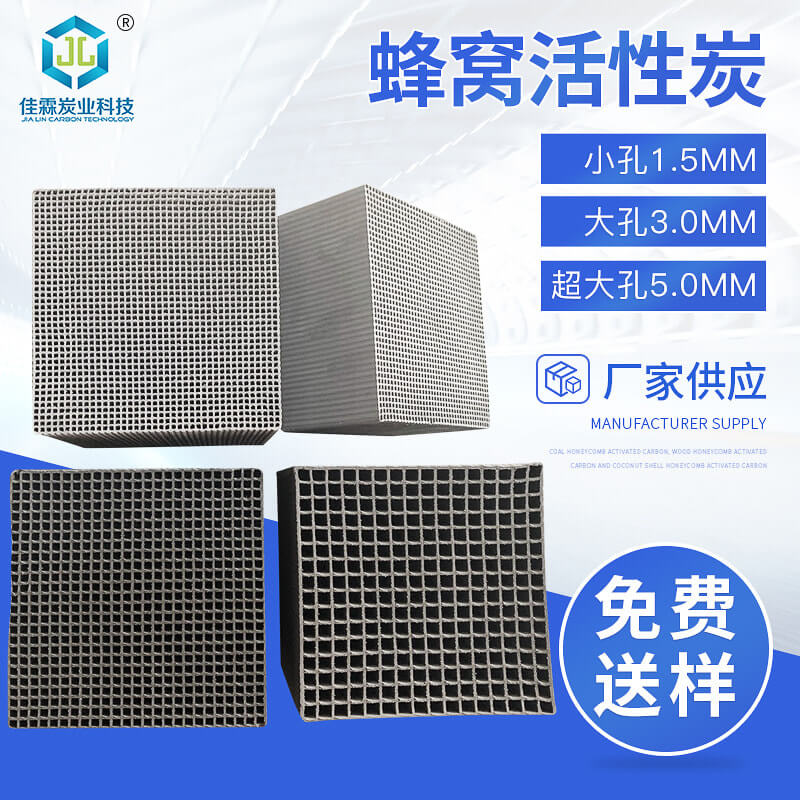
The manufacturing process of honeycomb activated carbon involves several specialized steps. We begin with high-quality raw materials, including coal, wood, or coconut shells, which undergo carbonization and activation processes. The activated carbon is then formed into a honeycomb structure with precise channel dimensions, typically 100mm × 100mm × 100mm or 150mm × 150mm × 150mm, with wall thicknesses ranging from 0.5mm to 1mm. This design ensures optimal contact between the contaminated air and the activated carbon surface while minimizing pressure drop across the filtration system.
Our state-of-the-art production facilities in Jiangxi, combined with strategic partnerships with manufacturers in Shanxi, Ningxia, Xinjiang, and Guangdong, enable us to maintain consistent quality and reliable supply even for large-scale industrial projects. Each batch of our honeycomb activated carbon undergoes rigorous quality testing to ensure it meets our exacting standards for iodine value, butane activity, and mechanical strength.
Comprehensive Product Range for Diverse Industrial Needs
While our honeycomb activated carbon remains a flagship product, Jiangxi Jialin Carbon offers a complete range of activated carbon solutions to address various industrial challenges:
- Granular Activated Carbon: Ideal for industrial water treatment applications including dechlorination, oil removal, and deep purification of drinking water and wastewater
- Columnar Activated Carbon: Specialized for air purification and organic solvent recovery in chemical, petrochemical, and pharmaceutical industries
- Coal-Based Activated Carbon: Effective for sewage treatment and waste incineration applications
- Wood-Based Activated Carbon: Preferred for water purification, food and beverage processing, metal extraction, and VOC治理 (VOC governance)
- Coconut Shell Activated Carbon: Features high mechanical strength, developed pore structure, and rapid adsorption capabilities
- Zeolite Molecular Sieves: Offers 40% higher efficiency than traditional activated carbon for organic waste gas treatment
This diverse product portfolio allows us to serve as a single-source supplier for all activated carbon needs, simplifying procurement and ensuring consistent quality across different applications. Our technical team works closely with clients to analyze their specific requirements and recommend the most suitable product or customized solution.
Technical Specifications of Our Honeycomb Activated Carbon
To help industrial buyers make informed decisions, we provide detailed specifications for our honeycomb activated carbon products:
| Parameter | Specification |
|---|---|
| Dimensions | 100×100×100mm or 150×150×150mm |
| Wall Thickness | 0.5-1.0mm |
| Iodine Value | ≥800-1000mg/g |
| Butane Activity | ≥12-15 |
| Bench Life | ≥5 years (when properly stored) |
| Operating Temperature | -20°C to 400°C |
These specifications demonstrate our commitment to producing honeycomb activated carbon that delivers consistent performance in demanding industrial environments. Our products are designed to withstand extreme temperatures and corrosive conditions while maintaining their structural integrity and adsorption efficiency over extended periods.
Industrial Applications of Honeycomb Activated Carbon
The versatility of our honeycomb activated carbon makes it suitable for numerous industrial applications where effective air purification or gas treatment is critical:
1. Organic Waste Gas Treatment: In chemical plants, coking plants, and other facilities generating volatile organic compounds (VOCs), our honeycomb carbon provides efficient adsorption of pollutants like benzene, toluene, xylene, and other hydrocarbons. The low pressure drop characteristic reduces energy consumption for air movement through the filtration system.
2. Solvent Recovery: Industries using organic solvents in their processes, such as printing, coating, and pharmaceutical manufacturing, can recover valuable solvents for reuse while preventing atmospheric emissions. Our honeycomb carbon’s high surface area ensures complete adsorption and easy regeneration for continuous operation.
3. Odor Control: Wastewater treatment plants, garbage disposal sites, and livestock farming operations use our honeycomb activated carbon to effectively neutralize unpleasant odors from hydrogen sulfide, ammonia, and other malodorous compounds.
4. Flue Gas Purification: Power plants, incinerators, and industrial boilers employ our products to remove heavy metals, dioxins, and other harmful substances from flue gases before emission, helping facilities comply with strict environmental regulations.
5. Air Purification in Confined Spaces: Subway stations, tunnels, and underground parking garages use our honeycomb carbon systems to maintain clean air quality by removing vehicle exhaust fumes and other pollutants.
For each application, our technical team provides comprehensive support, including system design, product selection, installation guidance, and maintenance protocols to ensure optimal performance and longevity of the filtration system.
FAQ
What makes honeycomb activated carbon different from other types?
Honeycomb activated carbon features a unique structure with parallel channels that provide large surface area for adsorption while maintaining low air resistance. This design makes it particularly effective for treating large volumes of air or gas with low contaminant concentrations, offering advantages in energy efficiency and operational costs compared to granular or powdered activated carbon systems.
How do I determine the right specifications for my industrial application?
Our technical team considers several factors including the type and concentration of contaminants, airflow rate, temperature, humidity, and space constraints. We typically recommend conducting pilot tests with different honeycomb carbon grades to determine the optimal product for your specific conditions. Our engineers can then design a complete filtration system tailored to your requirements.
What is the expected lifespan of honeycomb activated carbon in industrial applications?
The service life depends on several factors including contaminant type and concentration, operating temperature, humidity, and airflow velocity. Under typical conditions, our honeycomb activated carbon can last between 6 months to 3 years before requiring replacement or regeneration. We provide monitoring services to help you determine the optimal replacement schedule based on actual performance data.
Can honeycomb activated carbon be regenerated for reuse?
Yes, our honeycomb activated carbon can be regenerated through thermal or steam treatment processes that remove adsorbed contaminants and restore adsorption capacity. We offer regeneration services at our specialized facilities or can guide you in setting up on-site regeneration systems for large-scale applications. Proper regeneration can extend the useful life of the carbon by 3-5 cycles.
What quality certifications do your products have?
As a national high-tech enterprise, we maintain rigorous quality control systems certified to ISO 9001 standards. Our products comply with all relevant Chinese national standards (GB) and have been awarded the Jiangxi Province High-Quality Product designation. We can provide detailed test reports and certification documents for each batch of products upon request.
Summary
Jiangxi Jialin Carbon Technology Co., Ltd. stands as a premier manufacturer of honeycomb activated carbon and comprehensive industrial adsorption solutions. With our substantial production capacity, advanced manufacturing technology, and commitment to quality, we serve as a reliable partner for businesses worldwide seeking effective air purification and wastewater treatment solutions.
Our complete range of activated carbon products, including granular, columnar, coal-based, wood-based, coconut shell, and zeolite molecular sieves, allows us to address virtually any industrial filtration challenge. The strategic location of our production facilities and partner manufacturers ensures consistent supply and rapid delivery to customers across the globe.
By choosing Jiangxi Jialin Carbon as your activated carbon supplier, you gain access to not just high-quality products but also our technical expertise, custom solution development capabilities, and comprehensive after-sales support. We invite industrial buyers to contact us for personalized consultations and to discover how our activated carbon solutions can enhance your operational efficiency, reduce environmental impact, and contribute to sustainable business growth.