In the realm of industrial processes, the demand for efficient and reliable adsorption materials has never been greater. Whether it’s for water treatment, exhaust gas purification, or catalytic applications, the right choice of industrial adsorption materials can significantly enhance operational efficiency and environmental compliance. Jiangxi Jialin Carbon Tech Co., Ltd., a renowned national high-tech enterprise, stands at the forefront of this industry, offering a comprehensive range of activated carbon products tailored to meet diverse industrial needs.
Understanding Industrial Adsorption Materials
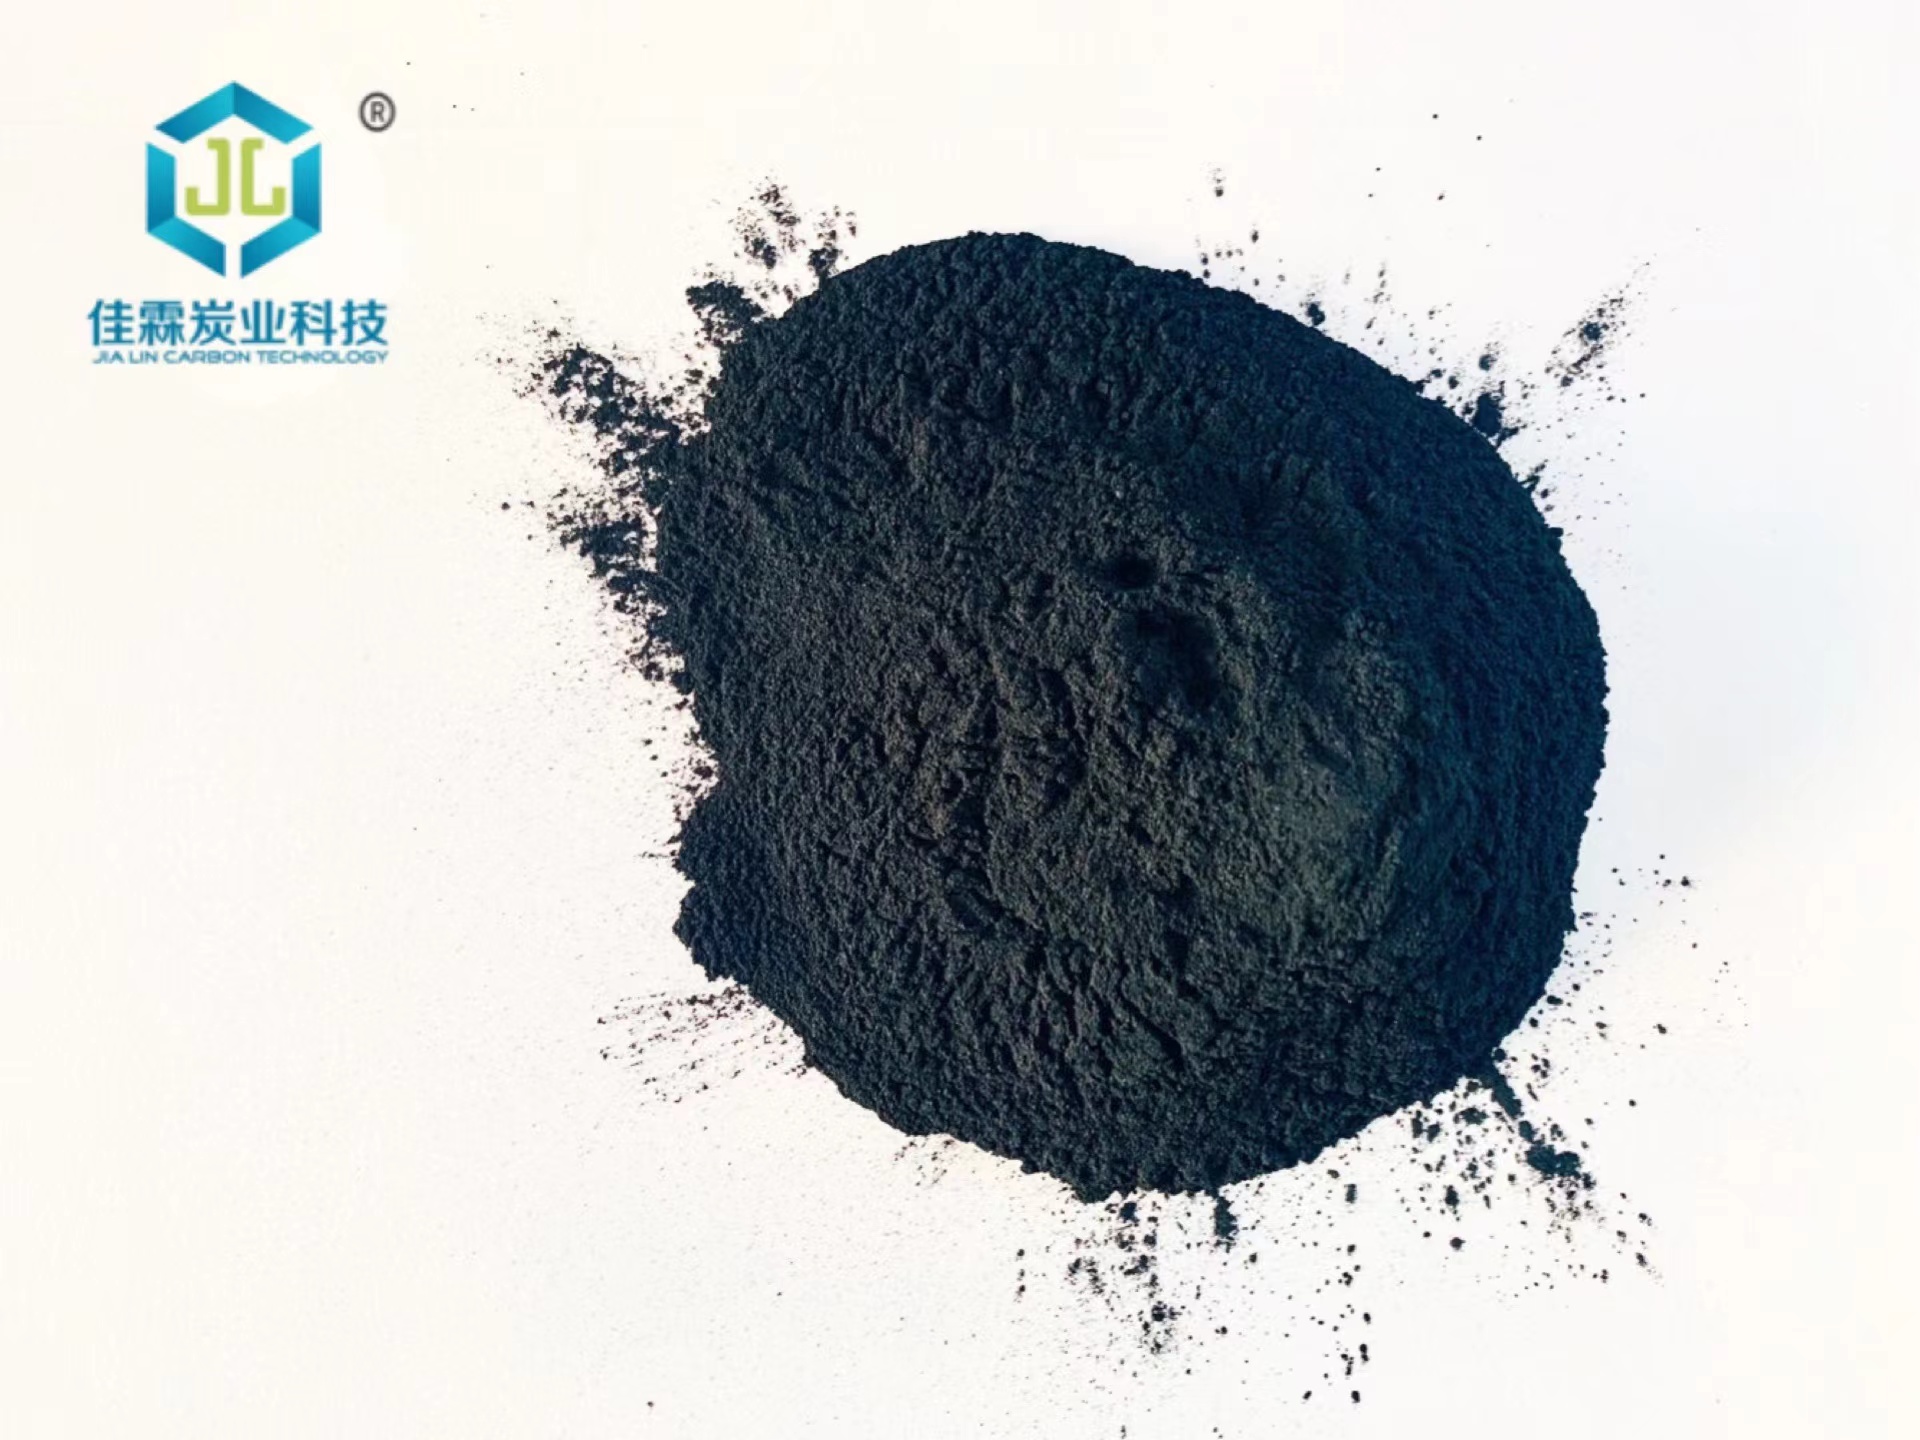
Industrial adsorption materials are substances that have the ability to attract and hold molecules of gases, liquids, or dissolved solids onto their surfaces. This property makes them invaluable in various industrial processes, including purification, separation, and catalytic reactions. Activated carbon, a highly porous form of carbon, is one of the most widely used industrial adsorption materials due to its exceptional surface area and adsorption capacity.
At Jiangxi Jialin Carbon Tech, we specialize in the research, production, and trade of activated carbon, offering a diverse product line that includes coal-based, wooden, coconut shell, honeycomb, and supercapacitor activated carbons. Each type is designed to excel in specific applications, ensuring optimal performance and cost-effectiveness for our clients.
Honeycomb Activated Carbon: The Ideal Solution for Exhaust Gas Purification
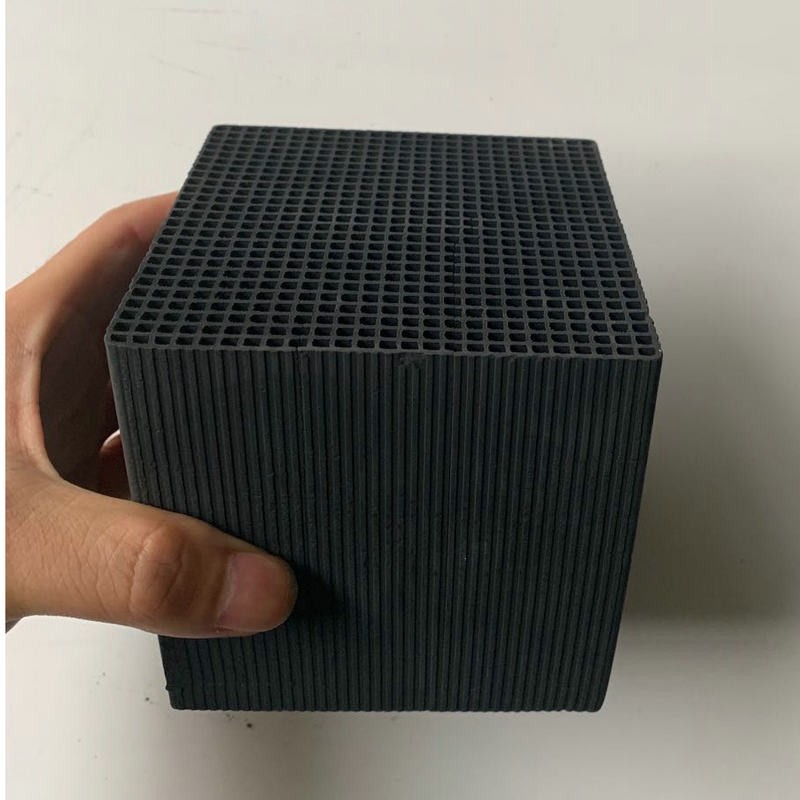
Honeycomb activated carbon is a standout product in our portfolio, renowned for its low wind resistance and high adsorption capacity during filtration. This makes it particularly suitable for purifying organic exhaust gases with high air volumes and low concentrations. Industries such as coking plants, chemical plants, printing and dyeing factories, plastic plants, and paper mills rely on honeycomb activated carbon to effectively treat their wastewater and exhaust gases, ensuring compliance with environmental regulations and minimizing their ecological footprint.
The unique structure of honeycomb activated carbon allows for efficient airflow while maximizing contact between the gas and the adsorption surface. This results in superior purification performance, even under challenging conditions. Additionally, our honeycomb activated carbon is designed for easy installation and maintenance, reducing downtime and operational costs for our clients.
Key Features of Honeycomb Activated Carbon
- Low wind resistance: Ensures efficient airflow through the purification system.
- High adsorption capacity: Effectively captures and retains pollutants from exhaust gases.
- Easy installation and maintenance: Simplifies system setup and reduces operational downtime.
- Durable construction: Withstands harsh industrial environments for long-lasting performance.
Granular Activated Carbon: The Preferred Choice for Water Treatment
Water treatment is another critical application area for industrial adsorption materials, where granular activated carbon plays a pivotal role. Our granular activated carbon products are designed to remove chlorine, oils, and other impurities from industrial water, as well as to provide deep purification of domestic drinking water and sewage. The porous structure of granular activated carbon allows it to effectively trap and remove contaminants, improving water quality and safety.
In addition to water treatment, granular activated carbon is also used in various other industrial processes, such as solvent recovery and air purification. Its versatility and effectiveness make it a valuable asset for industries seeking to enhance their operational efficiency and environmental performance.
Columnar Activated Carbon: Enhancing Air Quality and Solvent Recovery
Columnar activated carbon is another important product in our range, specifically designed for air purification and solvent recovery applications. Its unique shape and structure enable it to efficiently remove pollutants from the air, such as volatile organic compounds (VOCs) and other harmful substances. This makes it an ideal choice for industries that generate significant amounts of airborne pollutants, such as chemical plants and printing facilities.
Furthermore, columnar activated carbon is highly effective in recovering organic solvents like benzene, toluene, xylene, ethanol, gasoline, trichloromethane, and carbon tetrachloride. By capturing and reusing these valuable solvents, industries can reduce their operational costs and minimize their environmental impact. Our columnar activated carbon products are engineered to provide optimal performance in solvent recovery systems, ensuring high recovery rates and long service life.
| Activated Carbon Type | Primary Application | Key Advantage |
|---|---|---|
| Honeycomb Activated Carbon | Exhaust Gas Purification | Low wind resistance, high adsorption capacity |
| Granular Activated Carbon | Water Treatment | Effective removal of chlorine, oils, and impurities |
| Columnar Activated Carbon | Air Purification & Solvent Recovery | Efficient pollutant removal, high solvent recovery rates |
Coal-Based and Wooden Activated Carbon: Diverse Applications for Industrial Needs
In addition to honeycomb, granular, and columnar activated carbons, Jiangxi Jialin Carbon Tech also offers coal-based and wooden activated carbon products. Coal-based activated carbon is widely used in sewage treatment and waste incineration applications, where its high adsorption capacity and durability make it an ideal choice for capturing and removing pollutants. Wooden activated carbon, on the other hand, is preferred for water purification, food and beverage processing, and air purification due to its natural origin and excellent purification properties.
Our coal-based and wooden activated carbon products are manufactured using advanced processes and strict quality control measures to ensure consistent performance and reliability. Whether you need to treat industrial wastewater, purify drinking water, or improve air quality, our activated carbon solutions can meet your specific requirements and exceed your expectations.
Coconut Shell Activated Carbon: The Ultimate Choice for High-Performance Adsorption
Coconut shell activated carbon stands out for its exceptional mechanical strength, well-developed pore structure, large specific surface area, fast adsorption speed, high adsorption capacity, and ease of regeneration. These properties make it an ideal choice for demanding industrial applications where high-performance adsorption is required. Our coconut shell activated carbon products are engineered to provide superior performance in various applications, including water treatment, air purification, and solvent recovery.
The durability and longevity of coconut shell activated carbon also make it a cost-effective solution for industries seeking to minimize their operational costs and maximize their return on investment. By choosing our coconut shell activated carbon products, you can benefit from their exceptional performance and reliability, ensuring optimal results in your industrial processes.
Zeolite Molecular Sieve: A High-Efficiency Adsorption Material for Demanding Applications
In addition to our range of activated carbon products, Jiangxi Jialin Carbon Tech also offers zeolite molecular sieves, a high-efficiency adsorption material with no secondary pollution and the ability to be regenerated at high temperatures. Compared to similar activated carbons, zeolite molecular sieves offer a 40% increase in efficiency, making them an ideal choice for demanding applications such as adsorption, separation, catalysis, and environmental protection.
Zeolite molecular sieves are particularly suitable for treating organic exhaust gases with high air volumes and low concentrations, where their superior adsorption performance and durability can make a significant difference. Our zeolite molecular sieve products are designed to provide optimal performance in various industrial applications, ensuring efficient pollutant removal and compliance with environmental regulations.
FAQ
What are the main applications of industrial adsorption materials?
Industrial adsorption materials, such as activated carbon and zeolite molecular sieves, are primarily used for water treatment, exhaust gas purification, solvent recovery, air purification, and catalytic reactions. Their ability to attract and hold molecules of gases, liquids, or dissolved solids makes them invaluable in various industrial processes.
How does honeycomb activated carbon differ from other types?
Honeycomb activated carbon is characterized by its unique honeycomb structure, which provides low wind resistance and high adsorption capacity during filtration. This makes it particularly suitable for purifying organic exhaust gases with high air volumes and low concentrations, offering superior performance compared to other types of activated carbon.
What are the advantages of using granular activated carbon for water treatment?
Granular activated carbon is highly effective in removing chlorine, oils, and other impurities from industrial water, as well as providing deep purification of domestic drinking water and sewage. Its porous structure allows it to efficiently trap and remove contaminants, improving water quality and safety for various applications.
How can columnar activated carbon benefit solvent recovery systems?
Columnar activated carbon is designed to efficiently capture and recover organic solvents like benzene, toluene, xylene, ethanol, gasoline, trichloromethane, and carbon tetrachloride from industrial processes. By reusing these valuable solvents, industries can reduce their operational costs and minimize their environmental impact, making columnar activated carbon a valuable asset for solvent recovery systems.
Summary
Jiangxi Jialin Carbon Tech Co., Ltd. is a leading provider of high-quality industrial adsorption materials, specializing in activated carbon and zeolite molecular sieves for various industrial applications. Our comprehensive product line includes honeycomb, granular, columnar, coal-based, wooden, and coconut shell activated carbons, each designed to excel in specific applications and ensure optimal performance for our clients. With our advanced manufacturing processes, strict quality control measures, and commitment to innovation, we are dedicated to delivering superior adsorption solutions that meet the diverse needs of industries worldwide. Whether you need to treat water, purify air, recover solvents, or enhance catalytic reactions, Jiangxi Jialin Carbon Tech has the expertise and products to help you achieve your goals.